An anti reflective sapphire crystal coating should never be approved for bulk production on a verbal description alone. Before signing off, define the coating type and layer structure, the measurable reflectance and colour targets, the application method, the acceptance tests, and the operational terms. A written specification protects both buyer and manufacturer.
The cost of approving an under-specified coating
When a sourcing manager approves bulk production with nothing more than "AR coating, both sides" on a drawing, every downstream disagreement becomes a negotiation without a referee. Is the residual reflection measured as a single wavelength or a broadband average? Is a faint blue or violet tint an acceptable artefact of the coating stack or a rejection defect? Which surface carries the coating, and does the water-repellent outer layer sit above or below the anti reflective stack?
None of these questions can be answered after goods ship. They must be closed before the purchase order is released. The framework below gives you a repeatable structure for doing exactly that.
The COAT-OK framework for coating approval
C — Coating type and layer structure. Anti reflective performance comes from a stack of thin films, not a single layer. Define the intended layer count, whether the coating is broadband or tuned, and whether an additional oleophobic or hydrophobic outer layer is required. Confirm which surfaces are coated: outer only, inner only, or both. Two-sided coating reduces total reflection further but changes the visual signature and adds process steps; document the intended configuration explicitly.
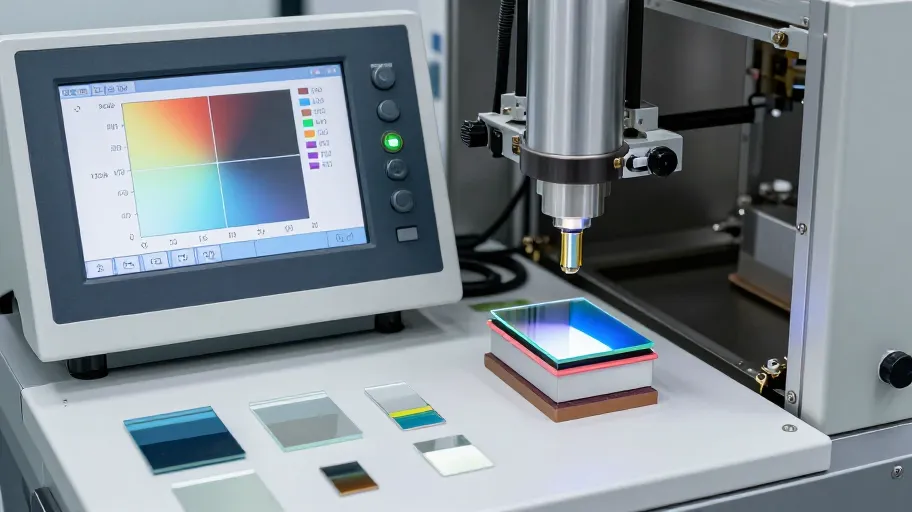
O — Optics definition. Specify reflectance as a measurable target across a stated wavelength range, plus any colour-appearance requirement. Verbal terms such as "low reflection" or "clear look" are not acceptance criteria. Agree how appearance will be judged: under what light source, at what angle, and against what reference sample.
A — Application method. Confirm the deposition process proposed for your parts and how it interacts with the substrate finish. The quality of an anti reflective sapphire crystal coating depends on the polish quality beneath it, so the crystal supplier and coating process must be aligned before production. Ask where the process runs, how batches are loaded, and how the supplier controls edge effects and fixtures marks.
T — Tolerance and testing. Agree the inspection plan: reflectance measurement, adhesion testing, abrasion resistance, humidity or salt exposure if your market requires it, and cosmetic criteria viewed at a stated distance and light. Define sampling method and the pass/fail rule. Ask what certificates or test reports can be provided for your project, and have the supplier confirm current evidence rather than assume it.
OK — Operational terms. Confirm in writing the sample policy, tooling or fixture arrangements, batch acceptance procedure, rework rules for coating failures, and how first-article approval relates to bulk release. These terms are project-specific; do not infer them from any prior project without written confirmation.
Coating configuration decision table
| Decision factor | Outer-only coating | Inner-only coating | Two-sided coating |
|---|---|---|---|
| Primary purpose | Reduce surface glare from ambient light | Reduce internal reflections and dial ghosting | Minimum total reflection |
| Visual signature | Strongest residual tint on the visible outer face | Subtle outward appearance | Combined stack appearance; verify colour |
| Outer surface exposure | Coated face faces wear and abrasion; confirm durability testing | Outer surface is uncoated sapphire | Both faces in play; verify outer-layer hardness |
| Process complexity | Fewest steps | Fewest steps with masking difference | Additional deposition run; confirm impact on yield and cost |
| Best suited when | Cost-sensitive models, glare control priority | Vintage-leaning aesthetics, reflections from dial are the complaint | Premium models where clarity is a headline feature |
| Must confirm with supplier | Abrasion test scope and outer-layer spec | Whether performance target is met with one coated face | Colour consistency across the batch and layer registration |
Use this table to narrow the configuration, then lock the choice into the drawing and specification sheet — not into an email thread.
Approval questions to resolve before bulk production
Coating and optics
- Which surfaces are coated, with how many layers, and is a topcoat included?
- What reflectance target applies, over what wavelength range, measured with which instrument?
- What colour-appearance standard governs acceptance, and is a signed reference sample retained by both parties?
Process and substrate
- What substrate polish specification is required for the coating process to perform as intended?
- Which deposition process will be used, and how are fixture marks and edge effects controlled?
- How will first articles be produced and approved relative to the bulk run?
Testing and inspection
- What adhesion, abrasion and environmental tests are included in the acceptance plan, and at what sampling level?
- What documentation accompanies each batch — measurement records, test reports, certificates — and in what form?
- What is the agreed procedure if a batch fails a cosmetic or optical criterion?
Commercial and operational terms
- What are the current sample policy, costs, lead arrangements and terms for this project? Confirm each directly in writing; none can be assumed from prior projects or general expectations.
The documentation gate: what "approved" should mean
Approval for bulk production should be a signed package, not a handshake. At minimum, the package should contain: the coating specification sheet referencing the drawing revision; the retained reference samples held by both parties; the inspection and test plan with pass/fail rules; and the first-article approval record tying the approved samples to the released production lot. If any element is missing, the honest status is "conditionally approved, specification pending" — and that status belongs on the record.
Pre-production approval checklist
- Coated surfaces and layer structure defined in the drawing
- Reflectance target, wavelength range and measurement method agreed
- Colour-appearance standard and retained reference samples signed
- Substrate polish specification aligned with the coating process
- Test plan agreed: adhesion, abrasion, environmental, cosmetic
- Sampling method and pass/fail rules documented
- Batch documentation requirements confirmed
- Sample policy, costs and terms confirmed in writing for this project
- First-article approval linked to bulk release in the PO terms
Frequently asked questions
Is two-sided anti reflective coating always the better choice? It depends on the model's positioning, the visual signature you want, and your durability requirements for the exposed outer face. Two-sided coating reduces total reflection further, but the decision should be made against the table above and verified with samples for your specific design.
How do I judge coating colour consistency across a batch? Agree a colour-appearance standard before production: a defined light source, viewing geometry, and a retained reference sample. Then define how much variation from that reference is acceptable, and record it in the specification.
What tests should an anti reflective coating specification include? At minimum, reflectance verification against the stated target, an adhesion test, an abrasion test appropriate to the exposed face, and any environmental exposure your market or brand standards require. The specific methods and pass criteria are project decisions to confirm with your supplier.
Can I approve bulk based on pre-production samples alone? Only if the samples are formally tied to the bulk release — same drawing revision, same process, documented first-article approval. Otherwise the samples prove the design intent but not the production lot.
Who is responsible if coating adhesion fails after delivery? Responsibility follows whatever was written before production. If the specification, test plan and failure-handling procedure were never documented, the outcome depends on negotiation rather than agreement. That is precisely why the specification gate exists.
Next steps
Confirm your coating specification. Send JadeZone Sapphire your drawing and target optical performance, and work through the COAT-OK questions above to lock a written specification before approving bulk production.
Low-friction option: download or copy the pre-production approval checklist above and use it as your internal review sheet — then bring the completed checklist to your specification discussion.